Racking & Shelving Specialists — Hamriyah Free Zone, Sharjah · Serving the UAE & GCC

Explore our range of heavy-duty industrial storage systems, gravity flow racks, cantilever frameworks, and structural wire mesh decking configured for automated intralogistics.
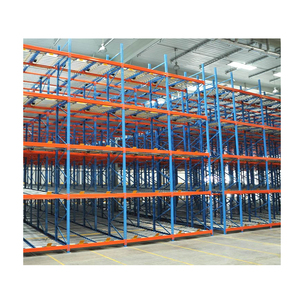
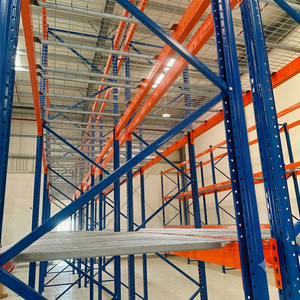
In modern industrial logistics, optimizing warehouse cubic space while accelerating stock throughput is a fundamental engineering challenge. Traditional selective racking systems offer 100% direct accessibility but sacrifice up to 60% of floor space to aisle clearance. Drive-in racking increases density but introduces operational risks, structural collision vulnerabilities, and severe throughput bottlenecks due to Last-In, First-Out (LIFO) limitations. Radio Shuttle Racking Systems—pioneered and refined by leading Chinese manufacturers—represent a paradigm shift in semi-automated and fully automated deep-lane storage dynamics.
A Shuttle Racking System utilizes an autonomous, self-powered shuttle car that travels on custom-engineered guide rails within dynamic storage channels. Operated via wireless radio frequency (RF) commands or integrated Warehouse Control Systems (WCS), the shuttle lifts, transports, and deposits unit loads (pallets) deep inside the racking structure. This eliminates the necessity for forklifts to enter the rack lanes, reducing pallet placement cycle times by up to 50% and protecting structural uprights from physical impacts.
As a leading Chinese manufacturer and global exporter, our engineering methodology relies on strict finite element analysis (FEA) and structural compliance under European FEM 10.2.02 (Design of Static Steel Pallet Racking) and American RMI (Rack Manufacturers Institute) specifications. Cold-formed steel profiles undergo rigorous tension, yield, and dynamic fatigue testing to guarantee performance under maximum dynamic loading conditions.
| System Parameter | Semi-Automated RF Shuttle | 2D Multi-Way Autonomous Shuttle | 4D Omni-Directional Shuttle AS/RS |
|---|---|---|---|
| Load Capacity Range | 500 kg – 1,500 kg per pallet | 1,000 kg – 1,500 kg per pallet | 800 kg – 2,000 kg per pallet |
| Max Travel Speed (Unloaded / Loaded) | 1.2 m/s / 0.8 m/s | 1.5 m/s / 1.0 m/s | 2.0 m/s / 1.2 m/s |
| Steel Grade Specifications | Q235B / Q355B Cold Rolled Steel | Q355B High-Tensile Structural Steel | Q355B / Custom Alloy Rails |
| Operating Temperature Thermal Range | -25°C to +45°C | -30°C to +50°C | -30°C to +50°C |
| Power Supply & Battery Tech | LiFePO4 (Lithium Iron Phosphate) 24V/48V | Supercapacitor + LiFePO4 Fast Charge | Inductive Wireless Power / LiFePO4 |
| System Software Interface | Handheld RF Remote / Basic PLC | WCS / WMS API via Wi-Fi / Industrial 5G | Fully Automated Cloud-WMS / AGV Stack |
When specifying high-density shuttle racking systems for global procurement, enterprise buyers must align system selection with specific operational constraints, inventory velocity, and environmental criteria:
Designed primarily for fast-moving consumer goods (FMCG), food and beverage distribution, and chemical warehousing where SKU volume is low but batch quantities are high. The semi-automated shuttle is positioned into the designated channel by a standard forklift. Once placed, the operator triggers the shuttle via an ergonomic remote control to execute loading, unloading, continuous picking, or tallying tasks. Beam profiles feature custom rolled-in lips that lock the shuttle guide rails securely, eliminating horizontal drift.
Cold storage operating costs are up to 5 times higher per square meter than ambient warehouses due to heavy electrical refrigeration loads. Shuttle systems engineered for cold chain facilities maximize thermal efficiency by compacting air volume. Key engineering adaptations include IP65-rated drive motors, low-temperature synthetic lubricants, anti-condensation internal heating elements, and thermal-insulated LiFePO4 battery packs equipped with intelligent Battery Management Systems (BMS).
For high-throughput, high-bay automated warehouses, 4-Way Shuttles can travel longitudinally and laterally across cross-aisles without requiring a dedicated crane or manual forklift repositioning. Integrated with vertical reciprocating lifts (elevators), 4-Way Shuttles form a complete 3D matrix AS/RS architecture, providing uninterrupted 24/7 autonomous material flow.
Procurement strategies for warehousing infrastructure are shifting away from standalone manual racking toward future-proof, automated frameworks. When sourcing shuttle systems from top Chinese manufacturers, global engineering teams prioritize the following technological developments:
Rooted in 36 years of industrial rack design, manufacturing precision, and global project execution across the UAE, GCC, Europe, and the Americas, our manufacturing ecosystem provides an end-to-end engineered service model:
Every engineering contract begins with a site survey analyzing structural slab capacity, seismic zones, floor flatness (FF/FL numbers), unit load dimensions, and SKU throughput velocity.
State-of-the-art continuous cold-roll forming mills, robotic laser welding centers, and automated electrostatic powder coating lines ensure structural tolerances within sub-millimeter margins.
100% compliance with ISO 9001:2015, CE certification, FEM 10.2.02, and RMI standards. Third-party material metallurgical testing certificates are provided with every export shipment.
Sourcing directly from China's leading shuttle racking manufacturer provides cost benefits, engineered structural precision, and customized automation integration. Speak directly with our senior intralogistics engineers today.
Send an Inquiry