Racking & Shelving Specialists — Hamriyah Free Zone, Sharjah · Serving the UAE & GCC

Factory-direct engineering featuring high-tensile Q235/Q355 steel, custom V-saddle geometry, modular stackability, and extreme weight capacities up to 50,000 kg.
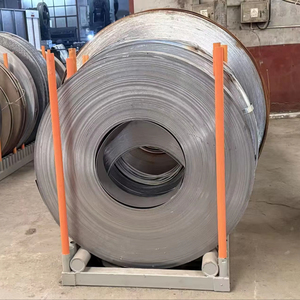
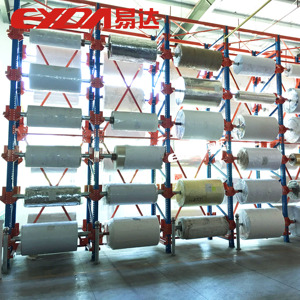
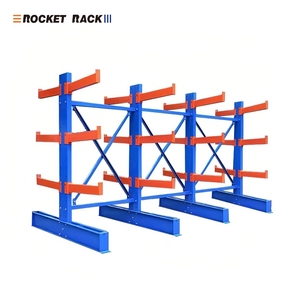
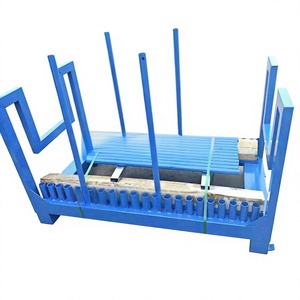
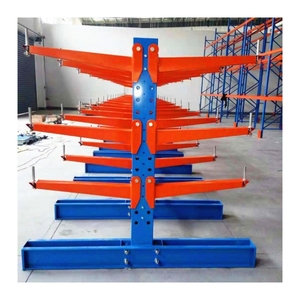
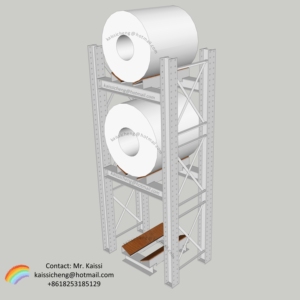
As a leading Chinese manufacturer and global exporter of heavy-duty heavy material handling equipment, our factory specializes in the structural engineering and mass fabrication of industrial coil storage racking systems. Storing cylindrical rolled metals—such as cold-rolled steel coils, hot-rolled steel plates, copper strip coils, aluminum coils, and wire rods—presents unique structural physics challenges. Unlike traditional palletized loads, steel coils concentrate massive deadweights onto concentrated point loads. Inadequate cradle geometry or sub-standard structural steel yields disastrous rack collapse, product coil deformation, and severe workplace safety hazards.
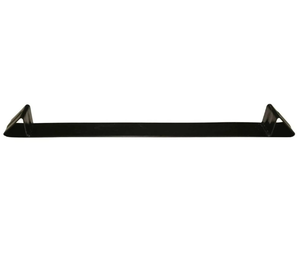
Our OEM/ODM manufacturing facility addresses these challenges through strict adherence to international metallurgical and structural standards (ISO 9001:2015, ANSI MH16.1, and EN 15512). Utilizing structural-grade structural steel channels (Q235B, Q355B, and ASTM A36), our coil racks incorporate reinforced V-shaped cradles, custom radius contact saddles, and anti-slip polyurethane (PU) or UHMW-PE protective linings to prevent coil surface indentation and roll-away accidents.
Every industrial coil rack system produced in our facility undergoes rigorous Finite Element Analysis (FEA) dynamic stress modeling. We simulate extreme load conditions, including static deadweight loading, impact loading during overhead crane drop-offs, and seismic acceleration forces. Our engineering framework ensures a conservative safety factor of 1.65 to 2.0 times the nominal working load limit.
| Engineering Specification | Standard Steel Coil Rack | Heavy-Duty Industrial Cradle Rack | Custom Multi-Tier Cantilever Coil System |
|---|---|---|---|
| Primary Material Grade | Q235B Structural Carbon Steel | Q355B / ASTM A572 Grade 50 Steel | Heavy Welded Structural I-Beams (Q355B) |
| Load Capacity Range | 5,000 kg – 15,000 kg per cradle | 15,000 kg – 35,000 kg per cradle | Up to 50,000 kg per rack bay |
| Contact Surface Lining | Heavy Powder Coating / Rubber Pad | Cast Polyurethane (PU) / Vulcanized Rubber | High-Density UHMW-PE Saddle Blocks |
| Coil Diameter Handling | 600 mm – 1,500 mm | 1,000 mm – 2,200 mm | Custom engineered to spec (up to 3,000 mm) |
| Surface Protection | Electrostatic Epoxy Powder Coat (60-80µ) | Thermosetting Powder Coat / Galvanized | Hot-Dip Galvanized (ASTM A123) for outdoor |
Our advanced manufacturing floor features automated robotic MIG welding bays operating under AWS D1.1 structural welding standards, CNC laser tube cutting, and 12-stage chemical pretreatment powder coating lines. This guarantees maximum resistance against corrosion, moisture, oil residue, and mechanical abrasion in harsh steel mill and logistics warehouse environments.
The global metal processing, automotive stamping, and heavy manufacturing industries are undergoing a massive transition toward automated logistics, high-density vertical space utilization, and green supply chain resilience. As procurement managers, warehouse operation directors, and supply chain executives evaluate prospective China wholesale manufacturers, several key macro trends are shaping the future purchasing strategies for steel coil storage racking:
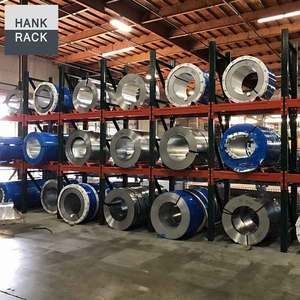
Historically, heavy steel coils were stored directly on timber skids or floor cradles ("Eye-to-Sky" or "Eye-to-Wall"). Modern industrial real estate costs have made single-level floor storage economically unsustainable. Industrial procurement is shifting heavily toward multi-tier stackable coil cradles and multi-level cantilever coil racking systems. Stacking coils vertically 3 to 5 levels high increases clear cubic storage efficiency by up to 300% while freeing valuable square footage for secondary slitting, stamping, and manufacturing operations.
Industry 4.0 smart warehousing requires coil storage racks to interface seamlessly with automated materials handling equipment. Future-proof coil racks now incorporate laser-guided entry locators, RFID asset-tracking plates, and standardized C-hook crane guide channels. Racks must maintain ultra-tight dimensional tolerances (+/- 1.5mm post-weld) to allow automated AGV forks and automated overhead C-hooks to lift and seat 25-ton coils without human intervention.
High-value surface-sensitive materials—such as automotive-grade pre-painted galvanized steel (PPGI), bright finish aluminum coils, and electrical silicon steel—cannot tolerate metal-on-metal contact. Scrap rates caused by surface scratches or pressure indentations can cost steel service centers hundreds of thousands of dollars annually. Procurement guidelines now demand custom-molded elastomeric Polyurethane or UHMW-PE liners integrated directly into the rack V-saddles.
Engineering innovations in high-strength metallurgy and modular fabrication have revolutionized how coil racks are constructed. The traditional approach of permanently welding monolithic frame structures is rapidly being superseded by modular, bolted-and-pinned adjustable frameworks that lower international freight costs and offer field reconfigurability.
Stackable steel coil cradles represent a major evolutionary leap in flexible storage. Utilizing heavy-square structural tubing legs terminating in target-type stacking cups, these units allow 3- to 4-high vertical stacking without requiring permanent floor-anchored rack uprights. When empty, the cradles can be nested together, drastically reducing empty warehouse footprint and simplifying inter-factory logistics transfer on flatbed trailers.
The geometric design of the support cradle is critical for distributing concentrated weight across the coil's circumferential curvature. Modern FEA studies demonstrate that an included saddle angle of 120 degrees provides optimal support for varying coil outer diameters (OD) ranging from 900mm to 2,000mm. This angle mitigates both horizontal outward rolling vector forces and excessive downward pinch-point stresses.
For installations in active seismic zones, industrial coil racks must feature heavy-duty floor baseplates anchored with chemical expansion bolts (such as Hilti HAS/HIT anchors). Structural engineers now incorporate energy-dissipating base gussets and cross-bracing channels that absorb crane positioning shocks and seismic lateral accelerations without structural fatigue or weld cracking.
Choosing the right manufacturing partner for heavy industrial material handling equipment is a critical decision that impacts operational safety, storage efficiency, and capital investment return. Our factory stands as a trusted supplier for global steel mills, coil slitting centers, automotive stamping facilities, and machinery OEMs worldwide.
• Direct Factory Pricing & Scale: Operating an expansive heavy industrial manufacturing plant with thousands of tons of monthly steel processing capacity, we eliminate intermediary trading markup, offering direct wholesale export pricing.
• Tailored Engineering Support: Our in-house engineering team provides 3D CAD modeling, BIM integration files, structural calculation reports, and customized color powder coating matching (RAL system) for complete project personalization.
• Global Export Compliance: Experienced in handling export documentation, CE conformity compliance, ISO certification, container loading optimization, and international shipping logistics to North America, Europe, the Middle East, Southeast Asia, and South America.