Racking & Shelving Specialists — Hamriyah Free Zone, Sharjah · Serving the UAE & GCC

Explore our precision-engineered OEM storage portfolios. From high-density automated gravity flow and stacker crane AS/RS configurations to bespoke modular steel assemblies, all systems undergo rigorous structural FEA testing and international quality certification.
As an industry-leading intralogistics manufacturer and exporter headquartered with premier production and distribution nodes in the Hamriyah Free Zone (HFZA), Sharjah, and state-of-the-art Asian manufacturing complexes, we deliver end-to-end engineered storage frameworks for clients across the UAE, GCC, Europe, and the Americas.
Unlike standard brokers or distributors, our fully integrated OEM infrastructure features continuous continuous-roll-forming mills, automated robotic MIG/TIG welding arrays, and custom multi-axis CNC punching suites. Every system is conceived through finite element structural analysis (FEA), calculating dynamic seismic loading, seismic shear stresses, and high-frequency cyclical fatigue to meet exacting international industrial standards including FEM 10.2.02, RMI, and EN 15512.
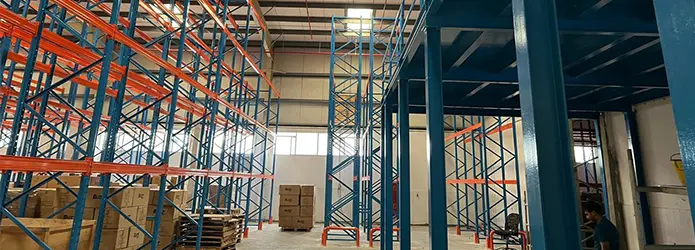
We source premier cold-rolled steel coils strictly compliant with high-tensile Q235B, Q355B, and SS400 metallurgies. Every coil batch undergoes yield tensile tests, chemical spectrometer verification, and ultrasonic flaw detection before continuous profiling.
Our cold roll-forming lines feature up to 26 active forming stages, maintaining an upright profile dimensional tolerance within ±0.5mm across 12-meter continuous sections—vital for high-bay stacker cranes and automated shuttles.
Turnkey integration with leading Warehouse Execution Systems (WES). We deliver plug-and-play fieldbus electrical hardware, photoelectric interlocks, automated guide rail assemblies, and seamless optical PLC communications.
Decades of international logistics engineering experience crystallized into an ironclad delivery methodology ensuring absolute alignment with your facility dimensions, floor slab tolerances, and throughput KPIs.
Comprehensive assessment of floor slab point loading, ceiling clear height, seismic zoning, dynamic pallet dimensional envelopes, SKU velocity profiles, and thermal variations (ambient to -30°C cold chain).
Iterative 3D CAD modeling, rack upright cross-sectional FEA stress simulations, crane aisle clearance calculations, and material flow route optimizations to ensure zero bottlenecking.
Automated roll-forming, robotic welding verification, multi-stage degreasing, electrostatic epoxy powder coating (60-80μm), and salt-spray corrosion chamber testing prior to secure export packing.
Deployment of certified engineering installation crews. Laser leveling alignment to TR34 / DIN 18202 standards, Hilti torque anchor fastening, and dynamic crane rail geometric calibration.
Full load-cell testing verification, issuance of stamped structural load plaques, operational operator safety training, and scheduled annual structural integrity lifecycle audits.
Review our primary structural configurations and automation compatibility indices. Sourced by global EPC contractors, warehouse developers, and operations managers worldwide.
| System Architecture | Optimal Handling Unit | Throughput Velocity | Vertical Utilization | Structural Steel Grade | Automation Interface |
|---|---|---|---|---|---|
| Automated AS/RS Pallet Racks | EUR/ISO/GMA Pallets (Up to 1,500kg) | Ultra High (>120 Pallets/hr) | Up to 40 Meters | Q355B High-Tensile Structural | Single/Double Deep Stacker Cranes |
| Carton & Pallet Gravity Flow (FIFO) | Totes, Cartons, Standard Skids | High Continuous Flow | Up to 12 Meters | Q235B / Cold-Rolled SPCC | Inbound Conveyors / AMR Induction |
| Radio Pallet Shuttle Systems | Deep-Lane High-Density Pallets | Medium-High Batched | Up to 24 Meters | Q355B Cold-Formed Rails | 2-Way / 4-Way Intelligent Shuttles |
| Heavy Duty Adjustable Pallet Rack | Selective Pallets, Varied SKUs | Standard Forklift Operational | Up to 16 Meters | Q235B Premium Coil | Reach Trucks, AGV Forklifts |
| Multi-Tier Mezzanine Platforms | Cartons, Hanging Garments, Bins | Multi-Level Manual / Conveyor | 2 to 4 Structural Levels | Heavy Universal Beams (UB/UC) | Vertical Reciprocating Conveyors |
| Industrial Cantilever Racking | Pipes, Extrusions, Timber, Barrels | Direct Crane / Side-Loader Access | Up to 9 Meters | Hot-Rolled I-Beam Columns | Side Loader / Automated Guided Tuggers |
How international procurement directors, supply chain leaders, and corporate engineering buyers are restructuring capital expenditures to navigate rapid robotics advances and supply chain volatility.
Modern enterprise sourcing looks far beyond the initial landed steel metric. Savvy procurement teams calculate total lifecycle wear-and-tear, floor deflection impact on automated vehicles, energy consumption profiles of regenerative crane hoists, and component standardized interchangeability over a 20-year operational lifecycle.
Global supply chain disruptions have driven tier-one enterprise buyers to bypass intermediary domestic traders in favor of direct engineering partnerships with verified OEM manufacturers. Direct OEM integration yields 25-35% material cost savings, direct access to metallurgists, and expedited custom structural roll-tooling.
Institutional investors and multinational corporations increasingly mandate Environmental Product Declarations (EPDs) for major racking installations. OEM exporters utilizing clean-energy blast-furnace processing, volatile organic compound (VOC)-free thermoset powder coatings, and zero-effluent pickling plants receive priority vendor scoring.
The confluence of artificial intelligence, high-density swarm robotics, and predictive sensor networks is redefining the structural engineering requirements of modern distribution centres.
Modern OEM projects now deploy dynamic 3D Digital Twins before metal is ever cut. Simulating 10,000+ continuous hours of picking cycles within virtual physics engines validates real-world deflection, acceleration g-forces, sensor handshake latency, and emergency stop impact envelopes down to millimeter tolerances.
Fixed-aisle stacker cranes are being augmented by agile 4-way multi-directional intelligent shuttles that traverse both cross-aisles and vertical high-speed lifts. These systems dynamically balance system workloads across the entire matrix, eliminating single-point mechanical crane failure risks.
The emergence of 'intelligent steel.' Sensorized baseplates and wireless strain gauges embedded directly into key upright nodes monitor dynamic seismic shifts, impact shocks from automated equipment, and ambient micro-vibrations, providing continuous predictive alerts to the central SCADA system.
Comprehensive engineering guidance to assist procurement executives, logistics developers, and technical project managers in finalizing custom OEM automated warehouse specifications.
We primarily utilize high-yield structural steel grades Q235B and Q355B (equivalent to European S235JR and S355JR / ASTM A572 Grade 50). Q355B is specifically specified for primary upright columns, heavy base plates, and guide rails subjected to intense cyclical dynamic fatigue, providing a minimum yield strength of 355 MPa and robust weldability without micro-fissuring.
Every custom system undergoes computerized structural static and dynamic Finite Element Analysis (FEA) calibrated to the project site's specific seismic spectral response acceleration parameters (Ss and S1). Our engineering calculation reports follow international seismic design provisions including RMI (Rack Manufacturers Institute) MH16.1, FEM 10.2.02, and European standard EN 16681, sizing column cross-sections and bracing trusses to safely dissipate seismic energy.
High-bay automated warehouses exceeding 20 meters in height demand rigid superflat flooring tolerances. Foundations must comply with DIN 18202 Table 3 Line 4 or Concrete Society TR34 'Defined Movement' specifications (DM1 or DM2). Tight slab tolerances prevent crane mast sway, ensure true verticality of rack upright arrays, and protect optical telemetry positioning systems from tracking errors.
Yes. As a pure OEM/ODM fabricator, we do not restrict clients to catalog norms. We custom-engineer beam connector brackets, heavy-duty load-support runners, drop-in pallet wire decking, and roll-profiled guide channels to house non-standard cargo, including automotive engine cradles, steel drums, cylindrical coils, oversized furniture skids, and bulk intermediate bulk containers (IBCs).
For temperatures down to -30°C, ordinary paint finishes can embrittle and chip, leading to rapid rust. We apply specialized low-temperature thermoset hybrid powders cured at precise thermal curves, or full continuous hot-dip galvanization conforming to ISO 1461 / ASTM A123. This creates a bonded metallurgical zinc-iron alloy barrier impervious to condensation cycling during defrost protocols.
Standard OEM high-bay racking systems (1,000 to 5,000 pallet positions) typically require 4 to 6 weeks for precision fabrication, roll-forming, automated robotic welding, and powder coating. Larger turnkey projects exceeding 20,000 positions generally run 8 to 12 weeks, managed via milestone batch releases to align seamlessly with the customer’s civil construction and maritime container schedules.
All upright columns, heavy-duty cross beams, and guide rails are strapped with high-tensile steel banding, wrapped in moisture-resistant UV-inhibiting polyethylene stretch film, and mounted on heavy timber runners for safe forklift dunnage. Critical structural connecting cleats, zinc-plated hardware, and electronic parts are packaged in hermetically sealed moisture-barrier crates with vapor-phase corrosion inhibitor (VCI) desiccant packs.
Yes. We deploy experienced, multilingual resident structural installation supervisors to client sites across the GCC, Europe, and global regions. Our engineers manage crane rail laser leveling, torque verification of chemical floor anchors, plumb-and-square tolerance alignments, and supervise comprehensive static and dynamic load testing prior to official WCS operational sign-off.